

Application Note | In-Line Quality Control
In-Line Roughness Inspection Using Chromatic Confocal Optics
Instant Error Detection with Triggered and Continuous Pass/Fail Roughness Thresholds

Research & Experimental Testing
Duanjie Li, Jonathan Thomas & Pierre Leroux
Visual Design & Editorial
Andrew Shore
Introduction
Surface roughness and texture is vital to the end-use of a product. Fast, quantifiable, and reliable inline inspection of the product surface ensures detecting the defective products immediately so as to determine the work conditions of the production line. It not only improves productivity and efficiency, but also reduces defect rates, re-work, and waste.
Why a Non-Contact Profiler Matters for In-Line Roughness Inspection
Surface defects derive from materials processing and product manufacturing. In-line surface quality inspection ensures the tightest quality control of the end products. The NANOVEA 3D Non-Contact Profilometers utilize chromatic confocal technology with a unique capability to determine the roughness of a sample without contact. Multiple profiler sensors can be installed to monitor the roughness and texture of different areas of the product at the same time. The roughness threshold calculated in real-time by the analysis software serves as a fast and reliable pass/fail tool.
ℹ️ Learn more about non-contact profilometry lab services and in-line feasibility studies.
Measurement Objective
In this study, the NANOVEA roughness inspection conveyor system equipped with a point sensor is used to inspect the surface roughness of the acrylic and sandpaper samples. We showcase the capacity of NANOVEA non-contact profilometer in providing fast and reliable in-line roughness inspection in a production line in real-time.
NANOVEA In-Line
Profilometer

Results and Discussion

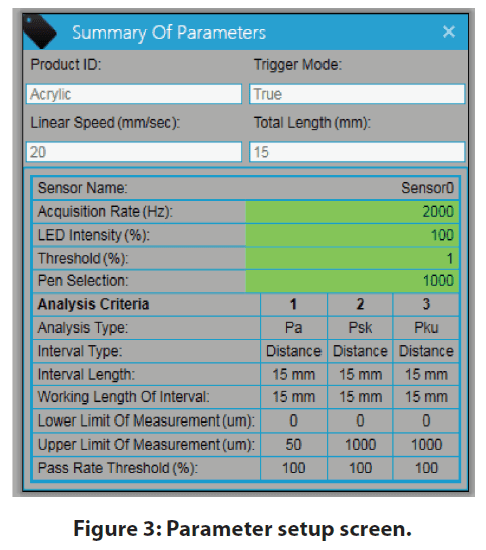
The conveyor profilometer system can operate in two modes, namely Trigger Mode and Continuous Mode. As illustrated in Fig. 2, the surface roughness of the samples are measured when they are passing under the optical profiler heads under the Trigger Mode. In comparison, Continuous Mode provides non-stop measurement of the surface roughness on the continuous sample, such as metal sheet and fabric. Multiple optical profiler sensors can be installed to monitor and record the roughness of different sample areas.

During the real-time roughness inspection measurement, the pass and fail alerts are displayed on the software windows as shown in Fig. 4 and Fig. 5. When the roughness value is within the given thresholds, the measured roughness is highlighted in green color. However, the highlight turns red when the measured surface roughness is out of the range of the set threshold values. This provides a tool for the user to determine the quality of a product’s surface finish.
In the following sections, two types of samples, i.e. Acrylic and Sandpaper are used to demonstrate the Trigger and Continuous Modes of the Inspection system.
| Parameter | Name | Definition |
|---|---|---|
| Pa | Arithmetical mean height | Mean surface roughness. |
| Pq | Root mean square height | Standard deviation of the height distribution, or RMS surface roughness. |
| Pp | Maximum peak height | Height between the highest peak and the mean plane. |
| Pv | Maximum pit height | Depth between the mean plane and the deepest valley. |
| Pz | Maximum height | Height between the highest peak and the deepest valley. |
| Psk | Skewness | Skewness qualifies the symmetry of the height distribution. A negative Ssk indicates that the surface is composed of mainly one plateau and deep and fine valleys. In this case, the distribution is sloping to the top. A positive Ssk indicates a surface with a lot of peaks on a plane. Therefore, the distribution is sloping to the bottom. |
| Pku | Kurtosis | Kurtosis qualifies the flatness of the height distribution. |
| Ppar | Projected area | Projected surface area. |
| Pdar | Developed area | Developed surface area. |
Table 1: Options of the roughness values for the pass/fail threshold.

Trigger Mode: Surface Inspection of the Acrylic Sample
A series of Acrylic samples are aligned on the conveyor belt and move under the optical profiler head as shown in Fig. 1. The false color view in Fig. 6 shows the change of the surface height. Some of the mirror-like finished Acrylic samples had been sanded to create a rough surface texture as shown in Fig. 6b.
As the Acrylic samples move at a constant speed under the optical profiler head, the surface profile is measured as shown in Fig. 7 and Fig. 8. The roughness value of the measured profile is calculated at the same time and compared to the threshold values. The red fail alert is launched when the roughness value is over the set threshold, allowing users to immediately detect and locate the defective product on the production line.


Continuous Mode: Surface Inspection of the Sandpaper Sample
Surface Height Map, Roughness Distribution Map, and Pass / Fail Roughness Threshold Map of the sandpaper sample surface as shown in Fig. 9. The sandpaper sample has a couple of higher peaks in the used part as shown in the surface height map. The different colors in the palette of Fig. 9C represent the roughness value of the local surface. The Roughness Map exhibits a homogeneous roughness in the intact area of the sandpaper sample, while the used area is highlighted in dark blue color, indicating the reduced roughness value in this region. A Pass/Fail roughness threshold can be set up to locate such regions as shown in Fig. 9D.
As the sandpaper continuously passes under the in-line profiler sensor, the real-time local roughness value is calculated and recorded as plotted in Fig. 10. The pass/fail alerts are displayed on the software screen based on the set roughness threshold values, serving as a fast and reliable tool for quality control. The product surface quality in the production line is inspected in situ to discover defective areas in time.


Conclusion
In this application, we have shown the NANOVEA Conveyor Profilometer equipped with an optical non-contact profiler sensor works as a reliable in-line quality control tool effectively and efficiently.
The inspection system can be installed in the production line to monitor the surface quality of the products in situ. The roughness threshold works as a dependable criteria to determine the surface quality of the products, allowing users to notice the defective products in time. Two inspection modes, namely Trigger Mode and Continuous Mode, are provided to meet the requirement for inspection on different types of products.
The data shown here represent only a portion of the calculations available in the analysis software. NANOVEA Profilometers measure virtually any surface in fields including Semiconductor, Microelectronics, Solar, Fiber, Optics, Automotive, Aerospace, Metallurgy, Machining, Coatings, Pharmaceutical, Biomedical, Environmental and many others.
Frequently Asked Questions About In-Line Roughness Inspection
Why inspect surface roughness in-line?
Surface roughness and texture are vital to the end use of a product. Fast, quantifiable and reliable in-line inspection detects defective products immediately, revealing the working condition of the production line, improving productivity and efficiency, and reducing defect rates, re-work and waste.
How does a non-contact profiler inspect roughness on a production line?
NANOVEA chromatic confocal sensors measure the surface without contact as products pass underneath. The analysis software calculates roughness in real time and compares it with set thresholds, showing a green pass or red fail alert for each result.
What is the difference between triggered and continuous mode?
In Trigger Mode, the roughness of discrete samples is measured as each passes under the profiler head. Continuous Mode measures non-stop on continuous material such as metal sheet and fabric, recording local roughness along its length.
Which roughness parameters can be used as pass/fail thresholds?
Profile height parameters such as Pa, Pq, Pp, Pv and Pz, the skewness Psk and kurtosis Pku, and the projected and developed areas Ppar and Pdar.
Can several areas of a product be monitored at once?
Yes. Multiple profiler sensors can be installed to monitor and record the roughness and texture of different areas of the product at the same time.
What did the demonstration show?
Sanded acrylic samples among mirror-finished ones triggered red fail alerts as they passed the sensor, and on a used sandpaper strip the continuous roughness record dropped below the threshold in the worn region, locating the defective area in situ.
